You know, in the fast-paced world of manufacturing, the demand for high-quality Industrial Lenses is really picking up. As companies around the globe look for reliable suppliers, China has definitely stepped into the spotlight. There are tons of Chinese firms that specialize in making top-notch lenses, suited to all sorts of industrial needs. These lenses are super important across different sectors — from automation and healthcare to security systems.
Brands like Sunny Optical and Kowa are leading the way with innovative solutions that really help boost efficiency. They also offer customization options, so you can get something tailored just for your project. But here’s the thing: not all lenses are created equal. Some might not live up to the same standards, so it’s really important to buy from reputable manufacturers if you want to avoid headaches later on.
When you're out there shopping around, keep an eye on things like optical clarity, how tough the lenses are, and whether they’re worth the price. Picking the right Industrial Lenses can seriously make a difference in the quality of your work. Do your homework, talk to trustworthy suppliers who have a good track record, and don't rush. In this ever-changing market, finding reliable partners is really the secret to staying ahead and succeeding.
Overview of Industrial Lenses and Their Importance in Global Markets
Industrial lenses play a critical role in various sectors, from manufacturing to automation. These lenses enhance machine vision systems, enabling precise monitoring and quality control. Their importance in global markets cannot be overstated. Industries increasingly rely on advanced imaging for efficiency and accuracy.
When choosing industrial lenses, buyers consider factors like resolution, aperture, and focal length. High-resolution lenses capture fine details, improving inspection processes. A wider aperture allows more light, which is vital in low-light environments. Global buyers must evaluate these features based on specific applications. However, some lenses may not meet high standards, leading to potential delays and quality issues.
Despite technological advancements, challenges remain in sourcing the right lenses. Variability in manufacturing standards can lead to disappointment. Therefore, buyers benefit from thorough research and expert guidance. Understanding the optical properties and their impact on different applications helps make informed decisions. It’s essential to balance cost with quality, as cheaper options often compromise performance.
Key Features to Consider When Choosing Industrial Lenses
When selecting industrial lenses, several key features stand out. Focal length plays a crucial role. It determines how much of the scene you can capture. A shorter focal length offers a wider field of view. Conversely, a longer focal length allows for more detail from a distance. Understanding these specifications can significantly impact the performance of your Industrial Camera Lenses.
Image quality matters greatly as well. Resolution, contrast, and color accuracy are vital for capturing precise details. Lens aberrations can distort images, so checking for these is essential. Additionally, consider the lens's build quality. Robust construction ensures longevity in industrial environments. Dust and moisture resistance can be beneficial too, especially in challenging settings.
Compatibility with your existing equipment is essential. Ensure the lens mounts correctly on your industrial camera. Different applications may require specific types of lenses. For instance, macro lenses are ideal for close-up work, while telephoto lenses excel in long-distance scenarios. This variety can make choosing the right lens complex. Reflecting on your specific needs will guide you to the right choice. Aim for balance between quality, budget, and functionality in industrial camera lenses.
Top Manufacturers of Industrial Lenses in China
China has established itself as a leading manufacturer of industrial lenses, catering to a global market. A recent report by the International Optical Industry Association indicates that the demand for
C Mount Industrial Lenses
is rising by 15% annually. This growth is fueled by advancements in fields like automation and surveillance. Chinese manufacturers are uniquely positioned to fulfill this demand due to their advanced technology and production capabilities.
Experts note that many factories focus on specific lens types, including wide-angle and telephoto. These lenses are crucial for various applications, including robotics and machine vision. In 2022, the Chinese lens market accounted for nearly 30% of the global supply. This impressive figure underscores the competitive edge that these manufacturers possess. However, challenges such as quality control and regional competition persist, demanding continuous improvement.
The variety offered by Chinese manufacturers can be both an advantage and a challenge for buyers. Many lenses are available at competitive prices, but not all meet international quality standards. Some manufacturers may struggle to maintain consistency, which can impact global buyers. Thus, while sourcing from China, diligence is necessary to ensure the choice of reliable industrial lens suppliers.
Product Comparison: Quality, Cost, and Performance of Lenses
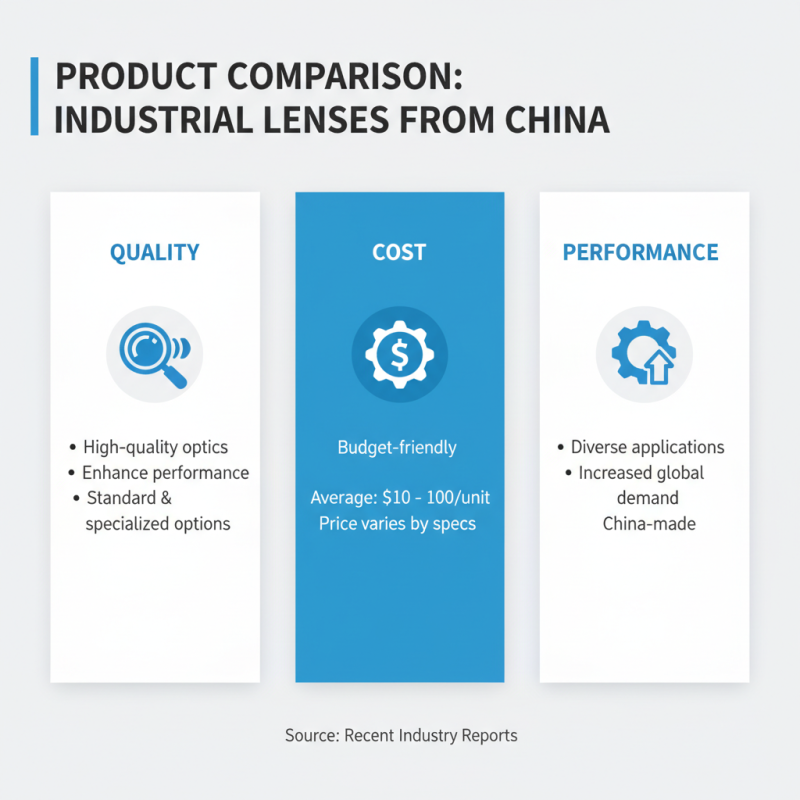
In recent years, the demand for industrial lenses has surged globally. Buyers seek high-quality optics that enhance performance while remaining budget-friendly. A comprehensive analysis reveals a diverse range of lenses produced in China. These include standard and specialized options catering to various applications. Recent industry reports indicate that the average cost of industrial lenses from China ranges from $10 to $100 per unit, depending on the specifications.
Quality remains paramount. Many lenses exhibit a high degree of clarity, durability, and precision. However, not all products meet rigorous industry standards. For instance, a study by the Optical Society highlighted that up to 20% of lenses may falter in stringent testing environments. Buyers often encounter inconsistencies in performance. This can impact their operations. Therefore, thorough vetting is essential before purchasing any lens.
Performance metrics are varied, with coatings and materials significantly affecting functionality. Some lenses offer superior light transmission, while others may boast enhanced scratch resistance. However, it’s crucial to acknowledge that cheaper options might compromise on these features. Buyers face a dilemma: balancing cost with performance. Investing in superior optics can lead to long-term savings and efficiency gains. Yet, it also poses the risk of over-investment in capabilities that may not be utilized.
Case Studies of Global Businesses Using Chinese Industrial Lenses
Chinese industrial lenses play a significant role in various global businesses. For instance, manufacturers in Europe have successfully integrated these lenses into their production lines. They enhance quality control processes, allowing for precise measurements in machinery.
Another case highlights how a North American company improved its imaging systems using Chinese Industrial Cameras Lenses. This led to a notable increase in efficiency. The lenses provided sharper images, ultimately resulting in better product outcomes. It wasn't all smooth sailing, however. Initial challenges included adapting software for compatibility.
In Asia, a leading tech firm adopted these lenses for their robotics. They focused on accuracy and speed during assembly lines. While they achieved impressive results, there were ongoing discussions about durability. Feedback suggested that some lenses required careful handling to maintain performance over time. These reflections indicate that while Chinese industrial lenses offer notable advantages, businesses should remain mindful of testing and adaptation.
Top 10 Industrial Lenses from China for Global Buyers
Future Trends in Industrial Lens Technology and Global Demand
The industrial lens market is evolving rapidly. According to industry reports, the global demand for high-quality lenses has surged by over 15% annually. This trend is driven by advancements in automation, robotics, and artificial intelligence. With these technologies, the need for precise imaging is more critical than ever.
Chinese manufacturers are stepping up their game in this sector. They are focusing on developing innovative lens designs that enhance performance and reduce production costs. Industry surveys indicate that over 70% of global buyers are looking for lenses that offer both affordability and quality. This shift suggests a balance between cost-efficiency and optical excellence.
However, challenges remain. Quality control is a persistent issue, impacting reliability. Many manufacturers struggle to maintain consistent production standards. Additionally, rapid technological advancements may outpace some companies, leading to potential gaps in innovation. As the market continues to grow, adapting to these changes is essential for success. The future of industrial lenses will require ongoing commitment to quality and responsiveness to market needs.
Tips for Sourcing Industrial Lenses from Chinese Suppliers
Sourcing industrial lenses from Chinese suppliers can be a rewarding experience. However, it requires careful planning and consideration. Start by identifying your specific needs. Determine the type of Industrial Light systems you plan to use. This helps narrow down your options and ensures you find suitable lenses.
Engage in thorough research on potential suppliers. Look for manufacturers with a track record of quality and reliability. Read reviews and seek testimonials. Building a relationship with suppliers can be beneficial, so maintaining open communication is key. Be mindful of language barriers. They might lead to misunderstandings about product specifications.
When evaluating lenses, don't overlook quality control measures. Ask about their testing processes. Ensure the lenses meet international standards. It’s easy to get caught up in price and overlook quality. Remember, a cheaper lens may not perform as well, leading to potential losses. Always prioritize quality over cost to ensure long-term satisfaction. Look for certifications that prove their product reliability. These are vital for any serious industrial light application.
FAQS
: Industrial lenses enhance machine vision systems, helping with precise monitoring and quality control across sectors.
Buyers need to evaluate resolution, aperture, and focal length for their specific applications and environments.
High-resolution lenses capture fine details, improving inspection processes and ensuring product quality.
Variability in manufacturing standards can lead to disappointment and quality issues for buyers.
China accounts for nearly 30% of the global industrial lens supply, showcasing its strong manufacturing capabilities.
The demand for high-quality lenses is rising over 15% annually, driven by automation and robotics advancements.
Buyers seek lenses that balance affordability with quality, indicating a need for cost-effective, high-performance options.
Many manufacturers struggle with quality control and maintaining consistent production standards, creating potential gaps.
Diligence is essential to ensure the selection of reliable suppliers that meet international quality standards.
Continuous commitment to quality and responsiveness to market changes will be crucial for success in lens technology.
Conclusion
Industrial lenses play a crucial role in various sectors, impacting global markets by enhancing operational efficiency and precision in manufacturing processes. This article outlines key features to consider when selecting industrial lenses, such as optical performance, durability, and compatibility with existing systems. It also highlights the leading manufacturers in China, showcasing how their lenses compare in quality, cost, and performance.
Furthermore, case studies illustrate the successful application of Chinese industrial lenses in global businesses, demonstrating their effectiveness in real-world scenarios. As the industry evolves, future trends indicate an increasing demand for advanced lens technologies, which could reshape sourcing strategies. The article concludes with practical tips for buyers looking to source industrial lenses from Chinese suppliers, ensuring that they make informed decisions to meet their specific needs.

 Compatible with 7.2mm-82mm chips
 High/Low Working Distance
 Aperture telecentric lens
 Measuring lens
 Maximum support 1.1" chips
 Maximum support 1.2" chips
 Maximum support 2/3" chips
 Long Working Distance
 CS mount Varifocal lens
 Varifocal board lens
 S mount lens
 Ring light
 UV/IR Light
 Bar light
 Arcuate high uniformity light
 Back light
 Flat light
 Collimated light
 Coaxial light
 Spot light
 Dome light
 Collimated Coaxial light
 Shadowless square light
 Scan light
 AOI light
 Analog controller
 Crossed-Roller Linear guide type
 Rotary Stages XRS series
 Stainless Steel Ball Bearing Linear Translation Stages
 Multi-axis Translation stages
 steel bar ball bearing stages
 Dovetail Type Rack&Pinion Positioning Stage
 Dovetail groove high-precision screw slide